Cold heading
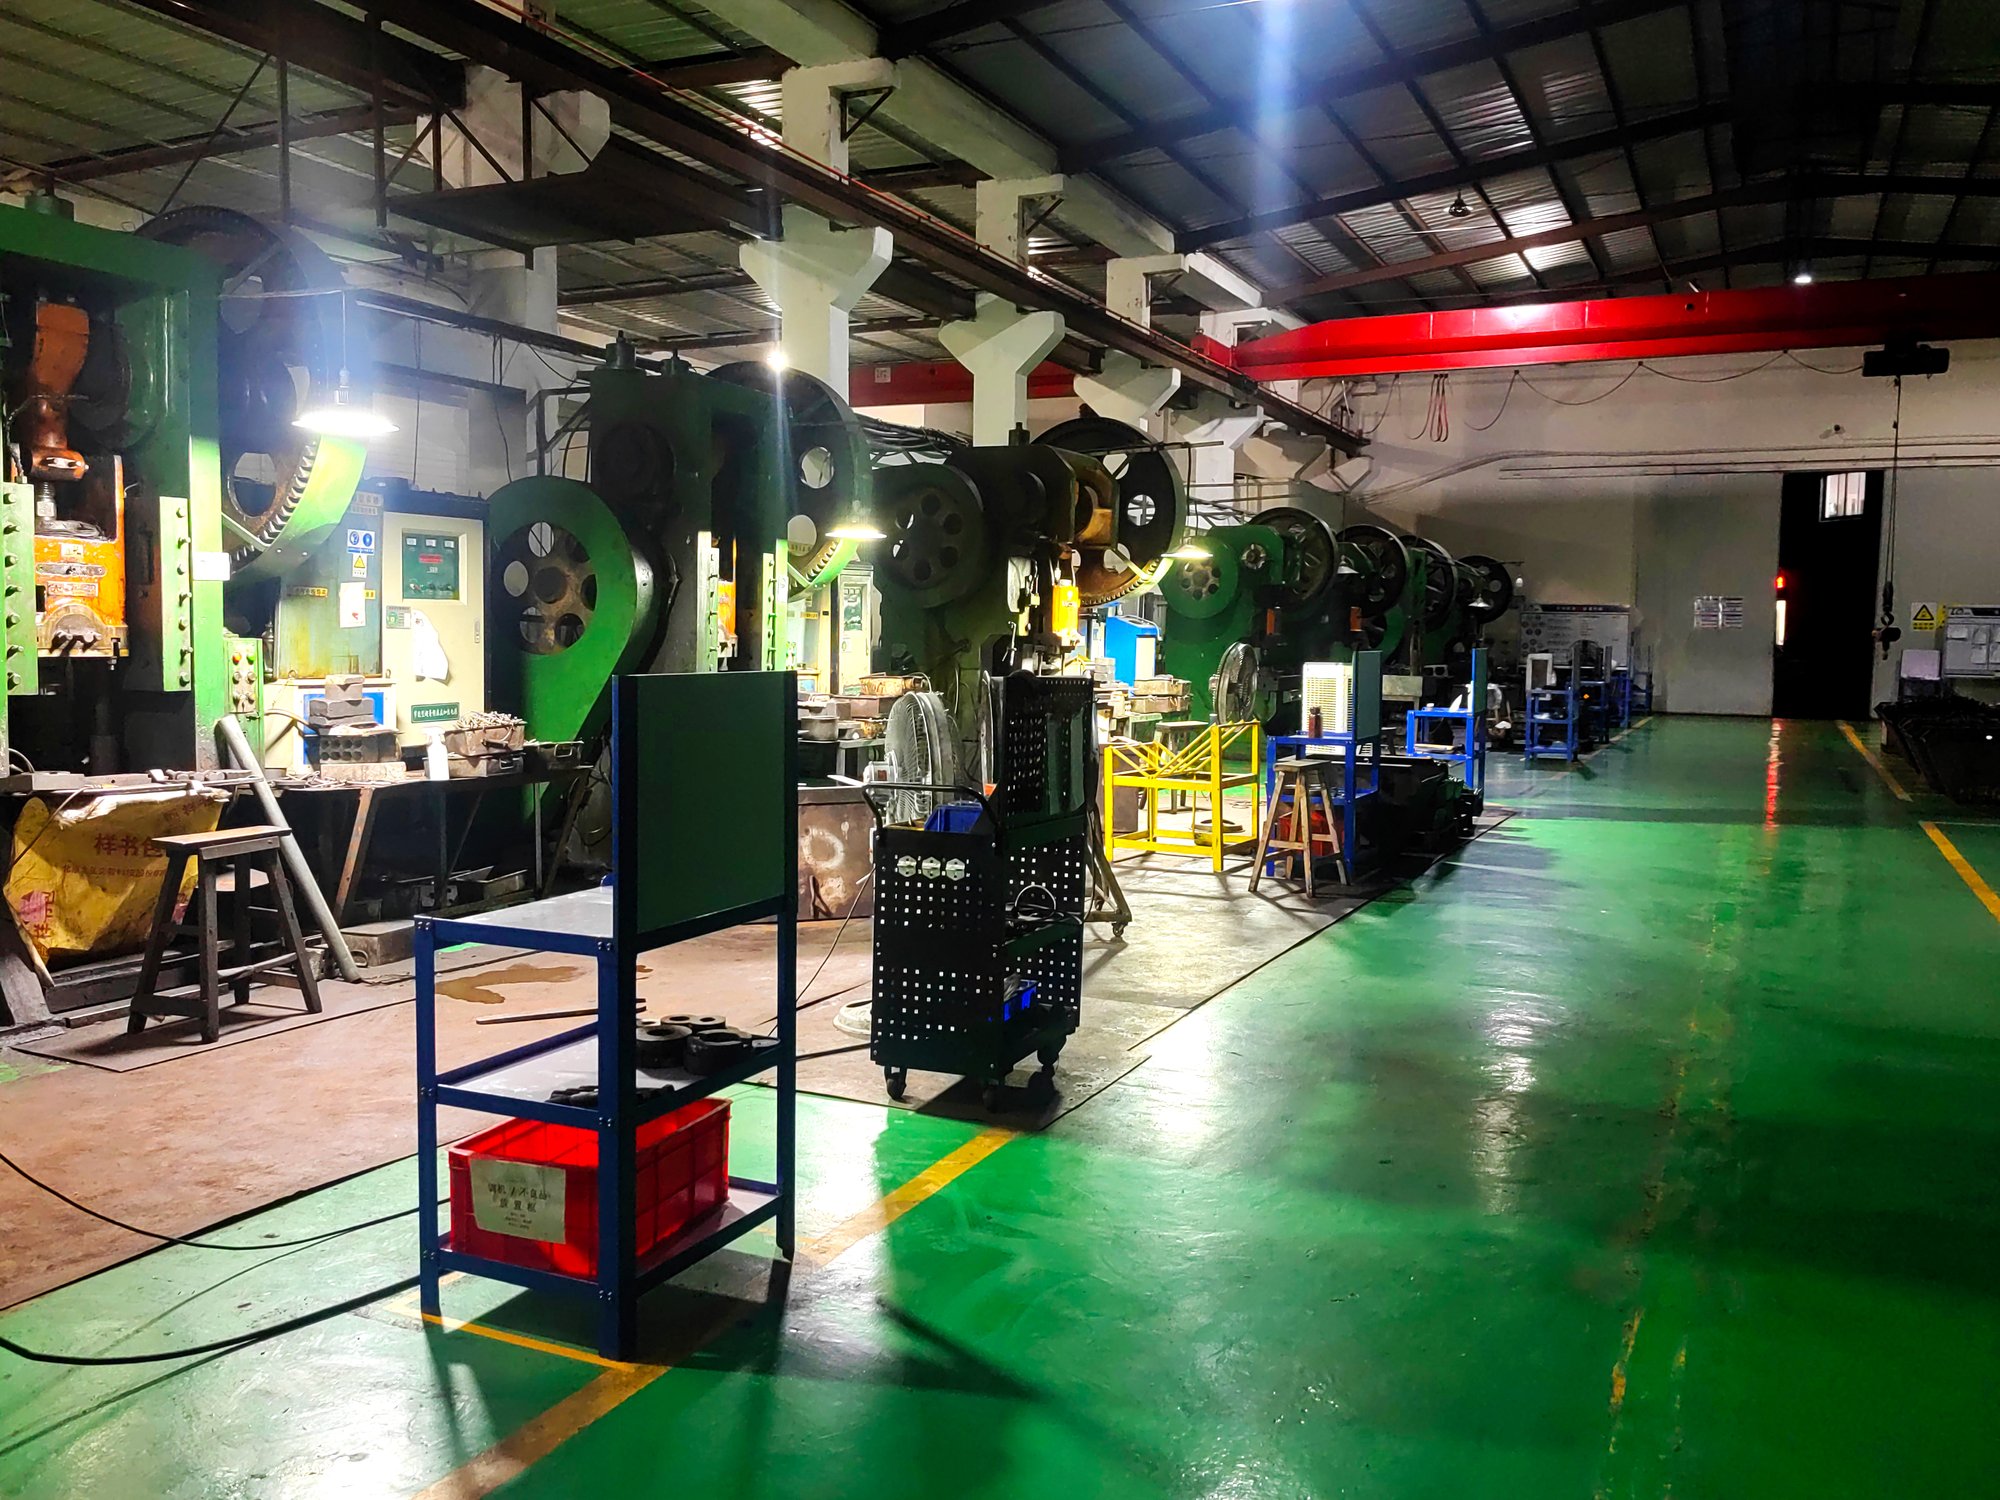
Multi-station cold heading forms the head, shoulder and rib in one pass. Wire is bought against mill certificate, heat number logged against every lot.
- M5 – M24
- Multi-station
- Heat-number traceable
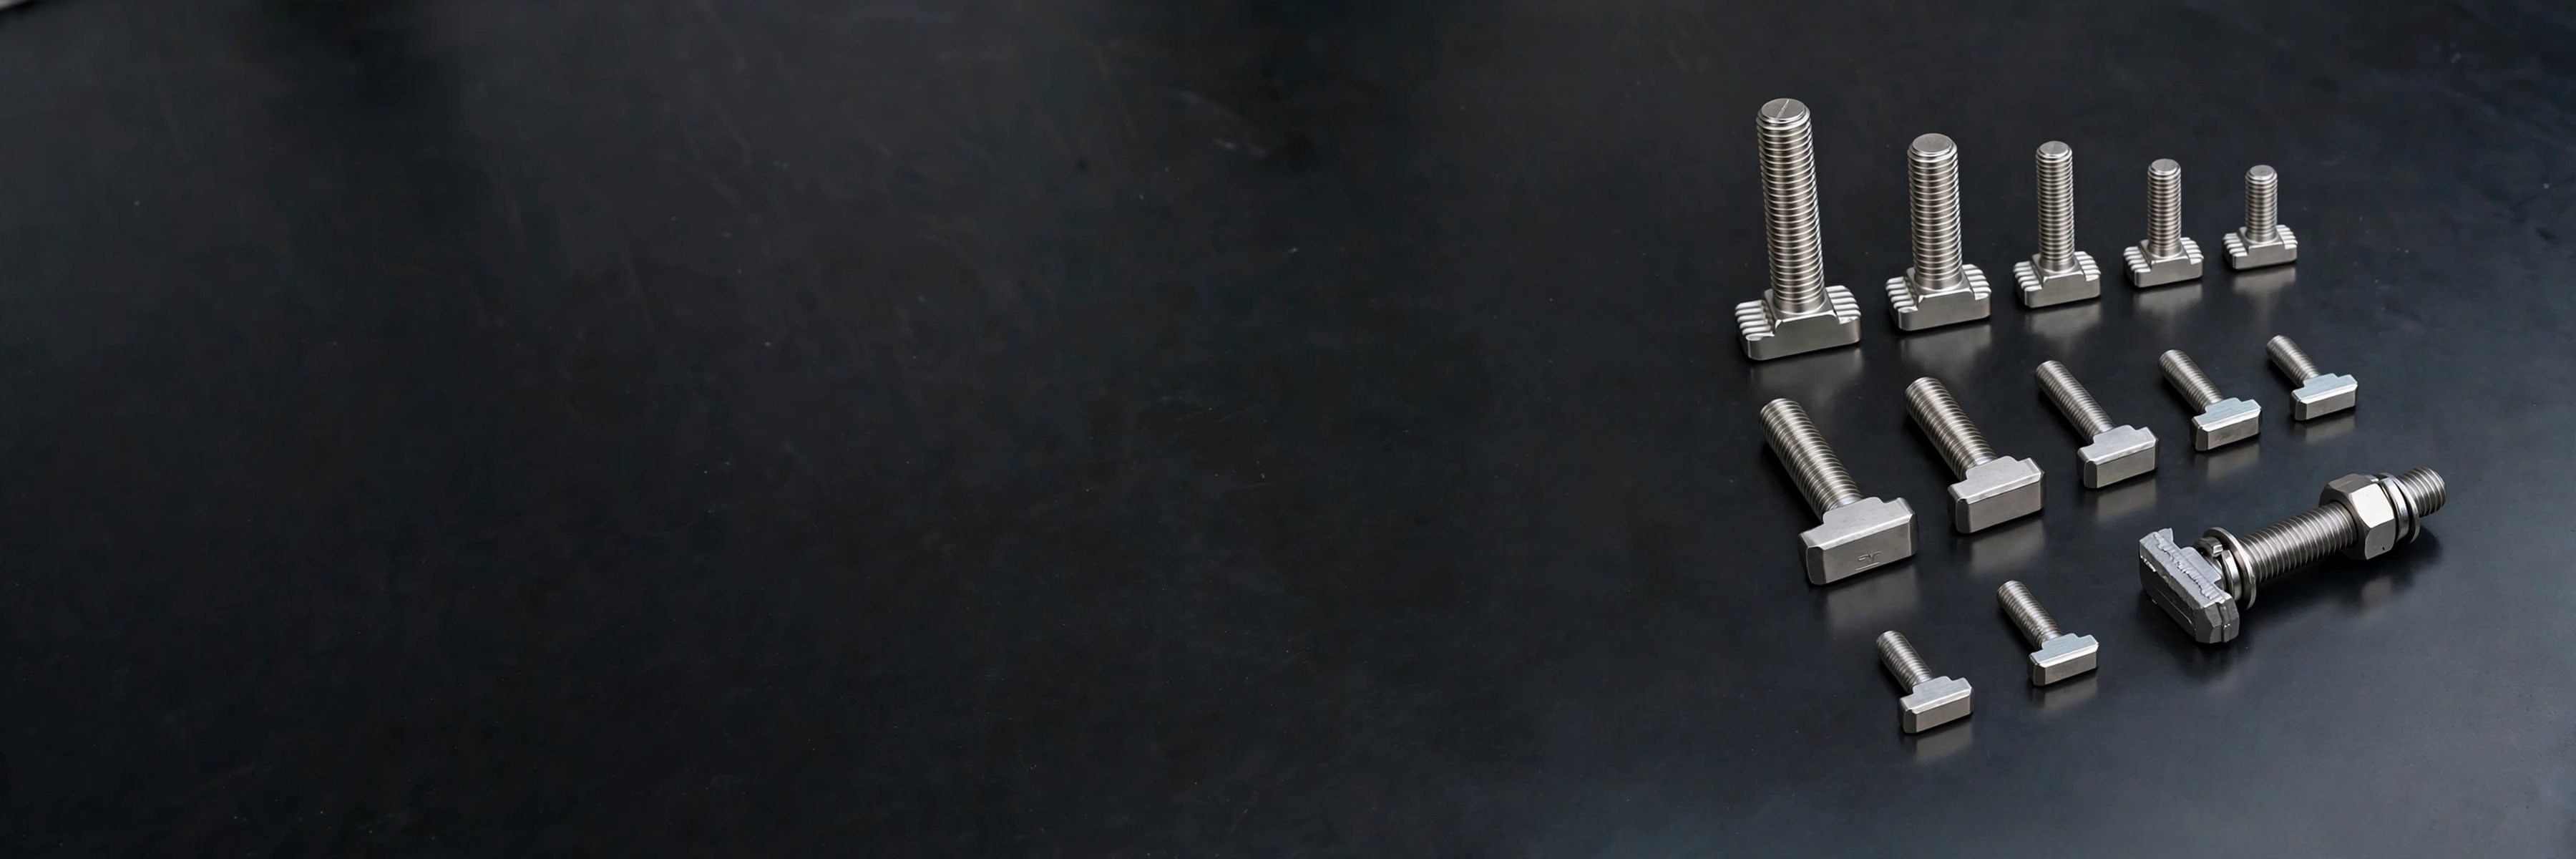
Non-standard T-bolt sets
Our main line: non-standard T-bolts, kitted with matching T-nuts and washers to your drawing — M5–M90, up to 3,000 mm. Standard T-bolts and general fasteners come off the same floor in Yuyao.
Three product lines
T-bolt, T-nut and washer kitted as one set and matched to your drawing — M5 to M90, lengths up to 3,000 mm.
Square neck, round neck and double-rib series, held in stock in the common sizes.
Hex bolts, nuts and washers, plus stamped and turned parts from the same floor.
FIG. 01 — T-BOLT SET
Capability — one roof
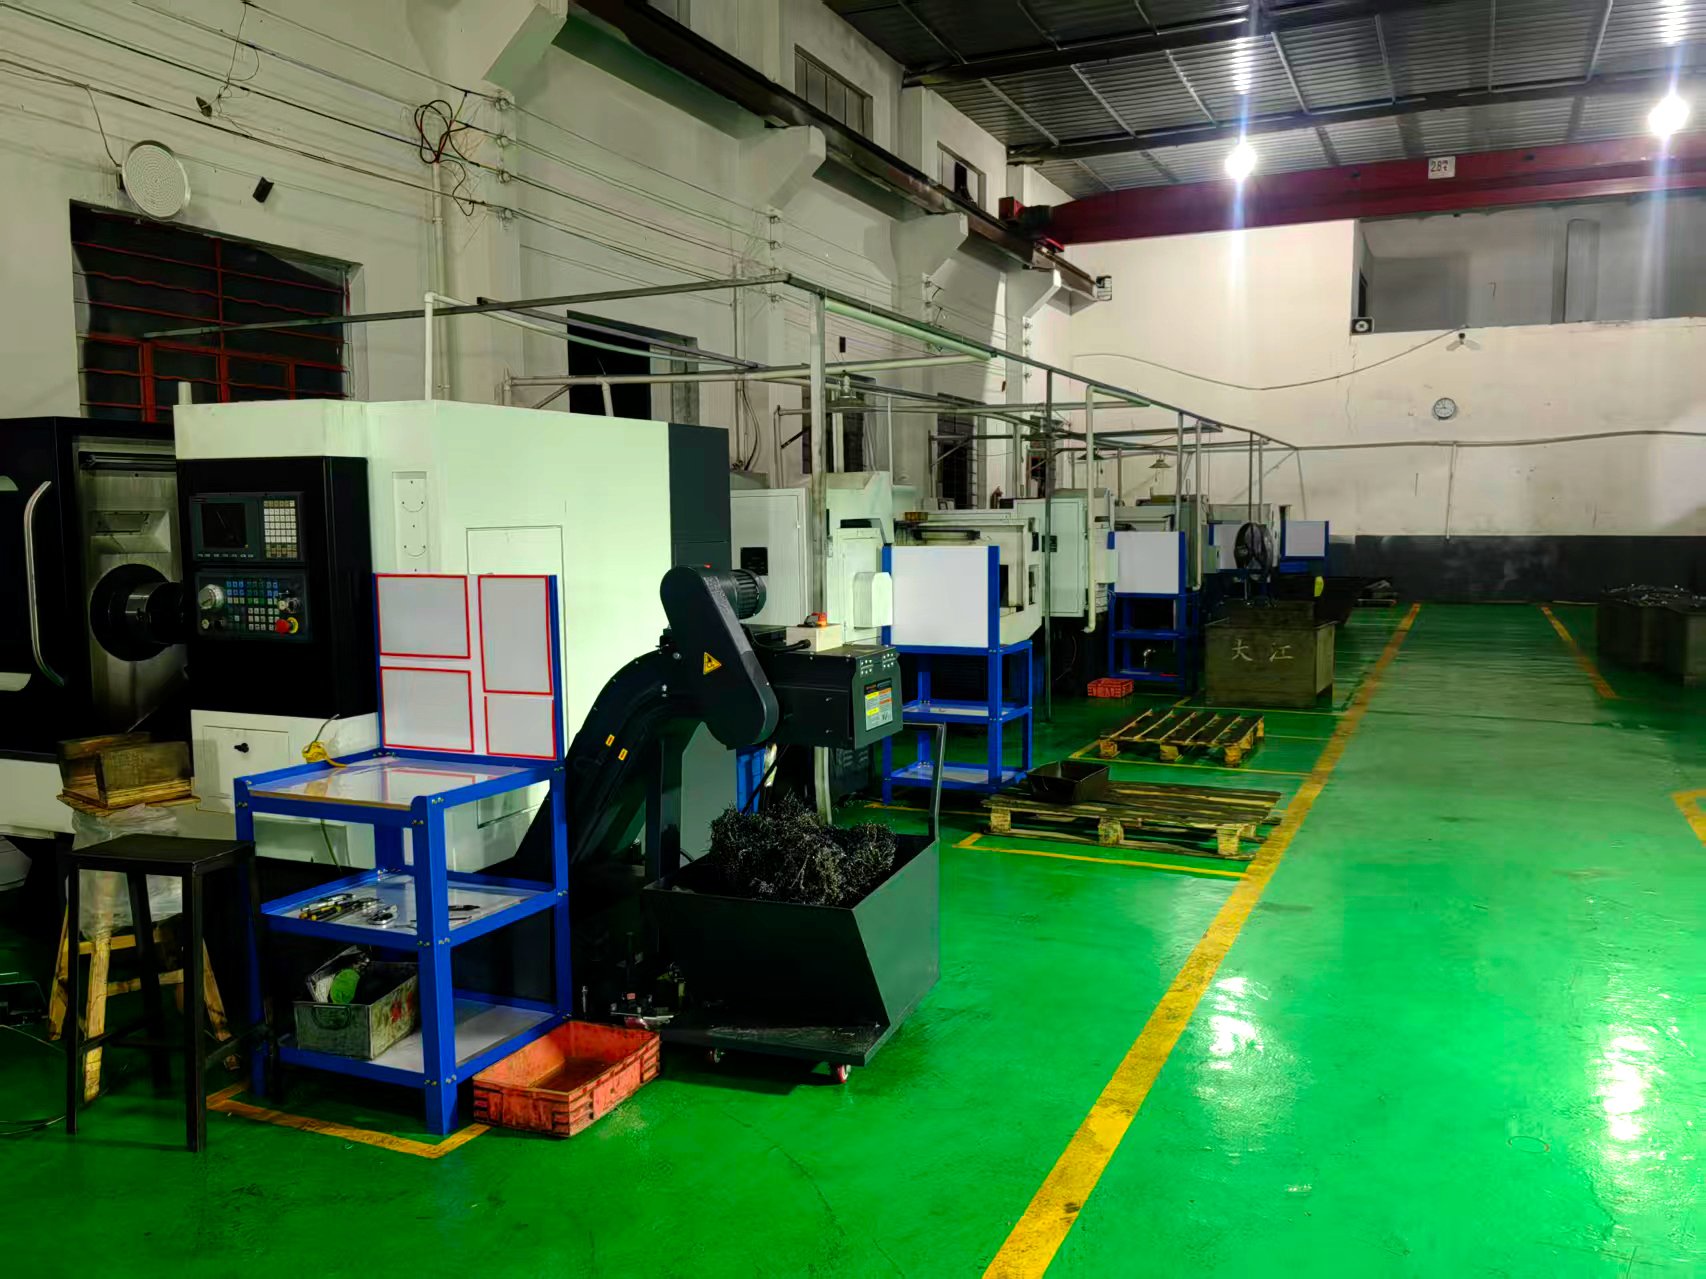
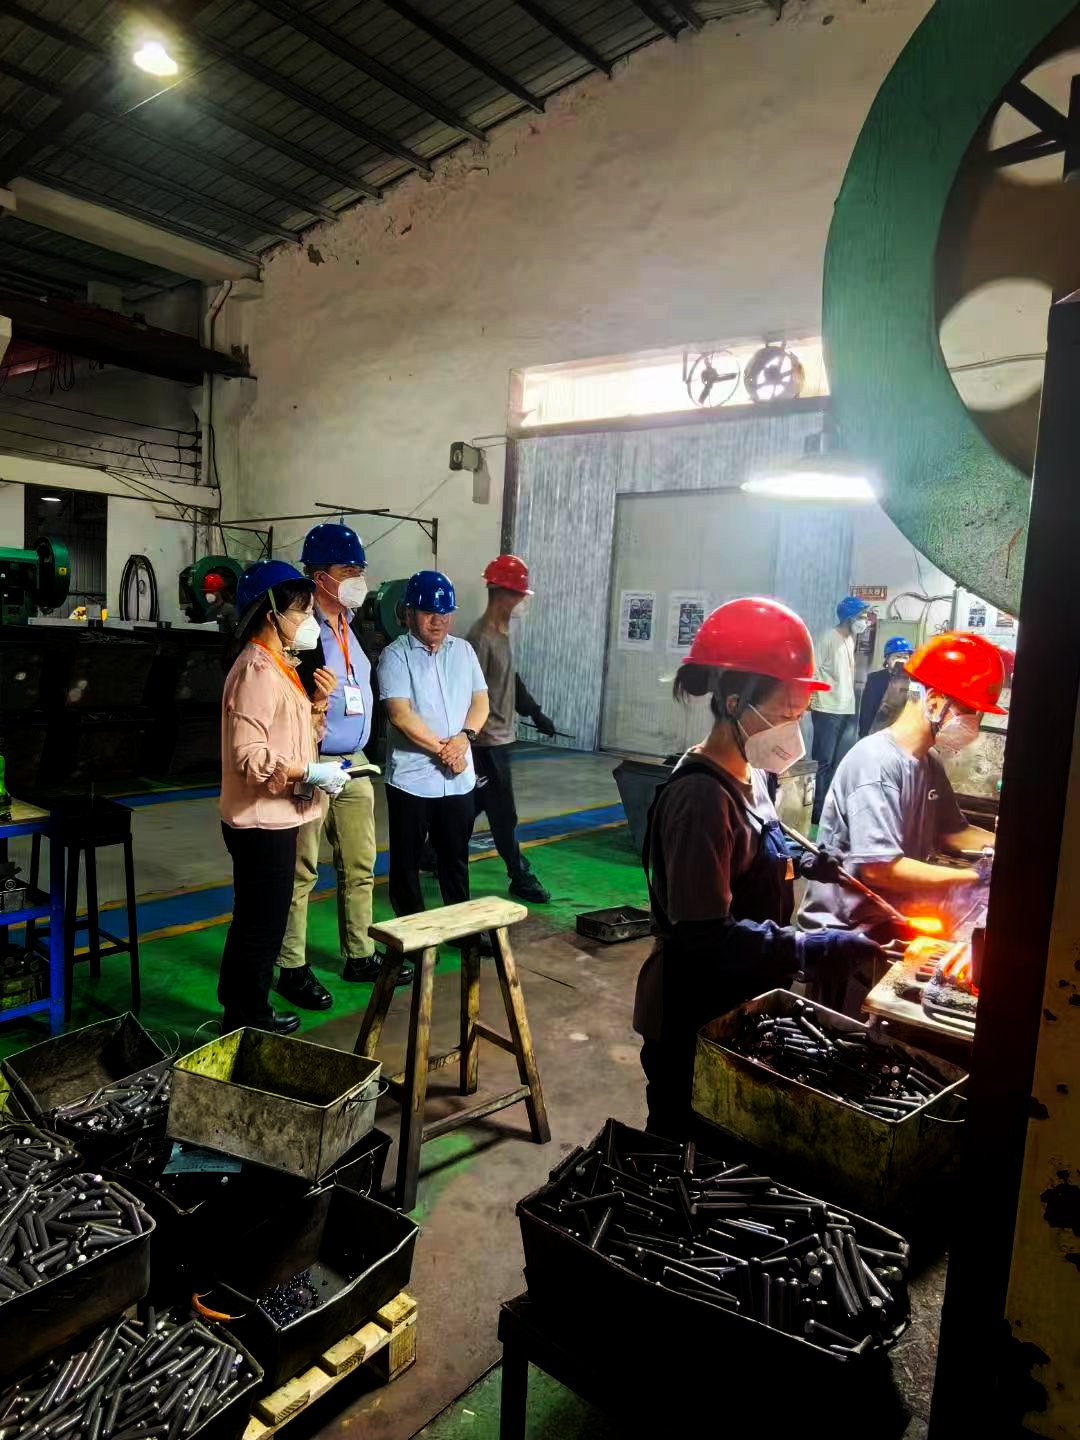
Forging, thread rolling, heat treatment and coating all happen inside the same fence. Nothing critical is subcontracted, which is why the batch records actually match the parts.
Plant & equipment →Multi-station cold heading forms the head, shoulder and rib in one pass. Wire is bought against mill certificate, heat number logged against every lot.
For large and extra-long parts — up to M90 and 3,000 mm — where cold forming runs out of press capacity. Grain flow follows the head geometry.
Rolled thread for fatigue-critical joints, CNC turning and milling for specials, lock plates and drawn components.
Quench and temper to classes 8.8 / 10.9 / 12.9 with hardness curve recorded per batch, no decarburised layer on the thread.
Hot-dip galvanising, zinc flake, DAC-type coatings and stainless systems specified by corrosivity category — C1 through CX.
Washer and nut pre-assembled onto the bolt, kitted per channel set, so the installer handles one part instead of four.
T-bolts and special fasteners
QA1 grade, production bolts
Hemudu, Yuyao — since 2005
Heavy-duty coating systems
Process — drawing to container
A lot number follows the wire coil through every station. If a customer asks which heat a carton came from, we answer in one query.
Coil received with mill cert, heat number logged.
Cold heading or hot forging of head and ribs.
Rolled to 6g — fatigue-critical, not cut.
Quench & temper, hardness curve recorded.
HDG / zinc flake / DAC, thickness mapped.
Fatigue, salt spray, hardness, 3.1 certificate.
Applications
Six sectors carry most of our volume. Each one has its own coating package, documentation set and inspection level.
T-bolts and special bolts for bogies, equipment cabins, skirt panels and track fastening — supplied into high-speed rail and metro programmes.
Safety-class fasteners with documented process control, material certificates and lot traceability for nuclear-grade bolting.
Blade bolts and high-tensile large-diameter bolts up to M90 in 42CrMoA, with heavy-duty coating for coastal and offshore duty.
Anchor and foundation bolts, embedded-channel T-bolts, lock plates and cast-in channel sets for precast and steel structures.
Truck T-bolts and non-standard automotive parts under IATF 16949 process control, with PPAP documentation where required.
Progressive-die stamping, hinges, brackets and assemblies — plus cabinet, tool-box and skirt locks.
Quality
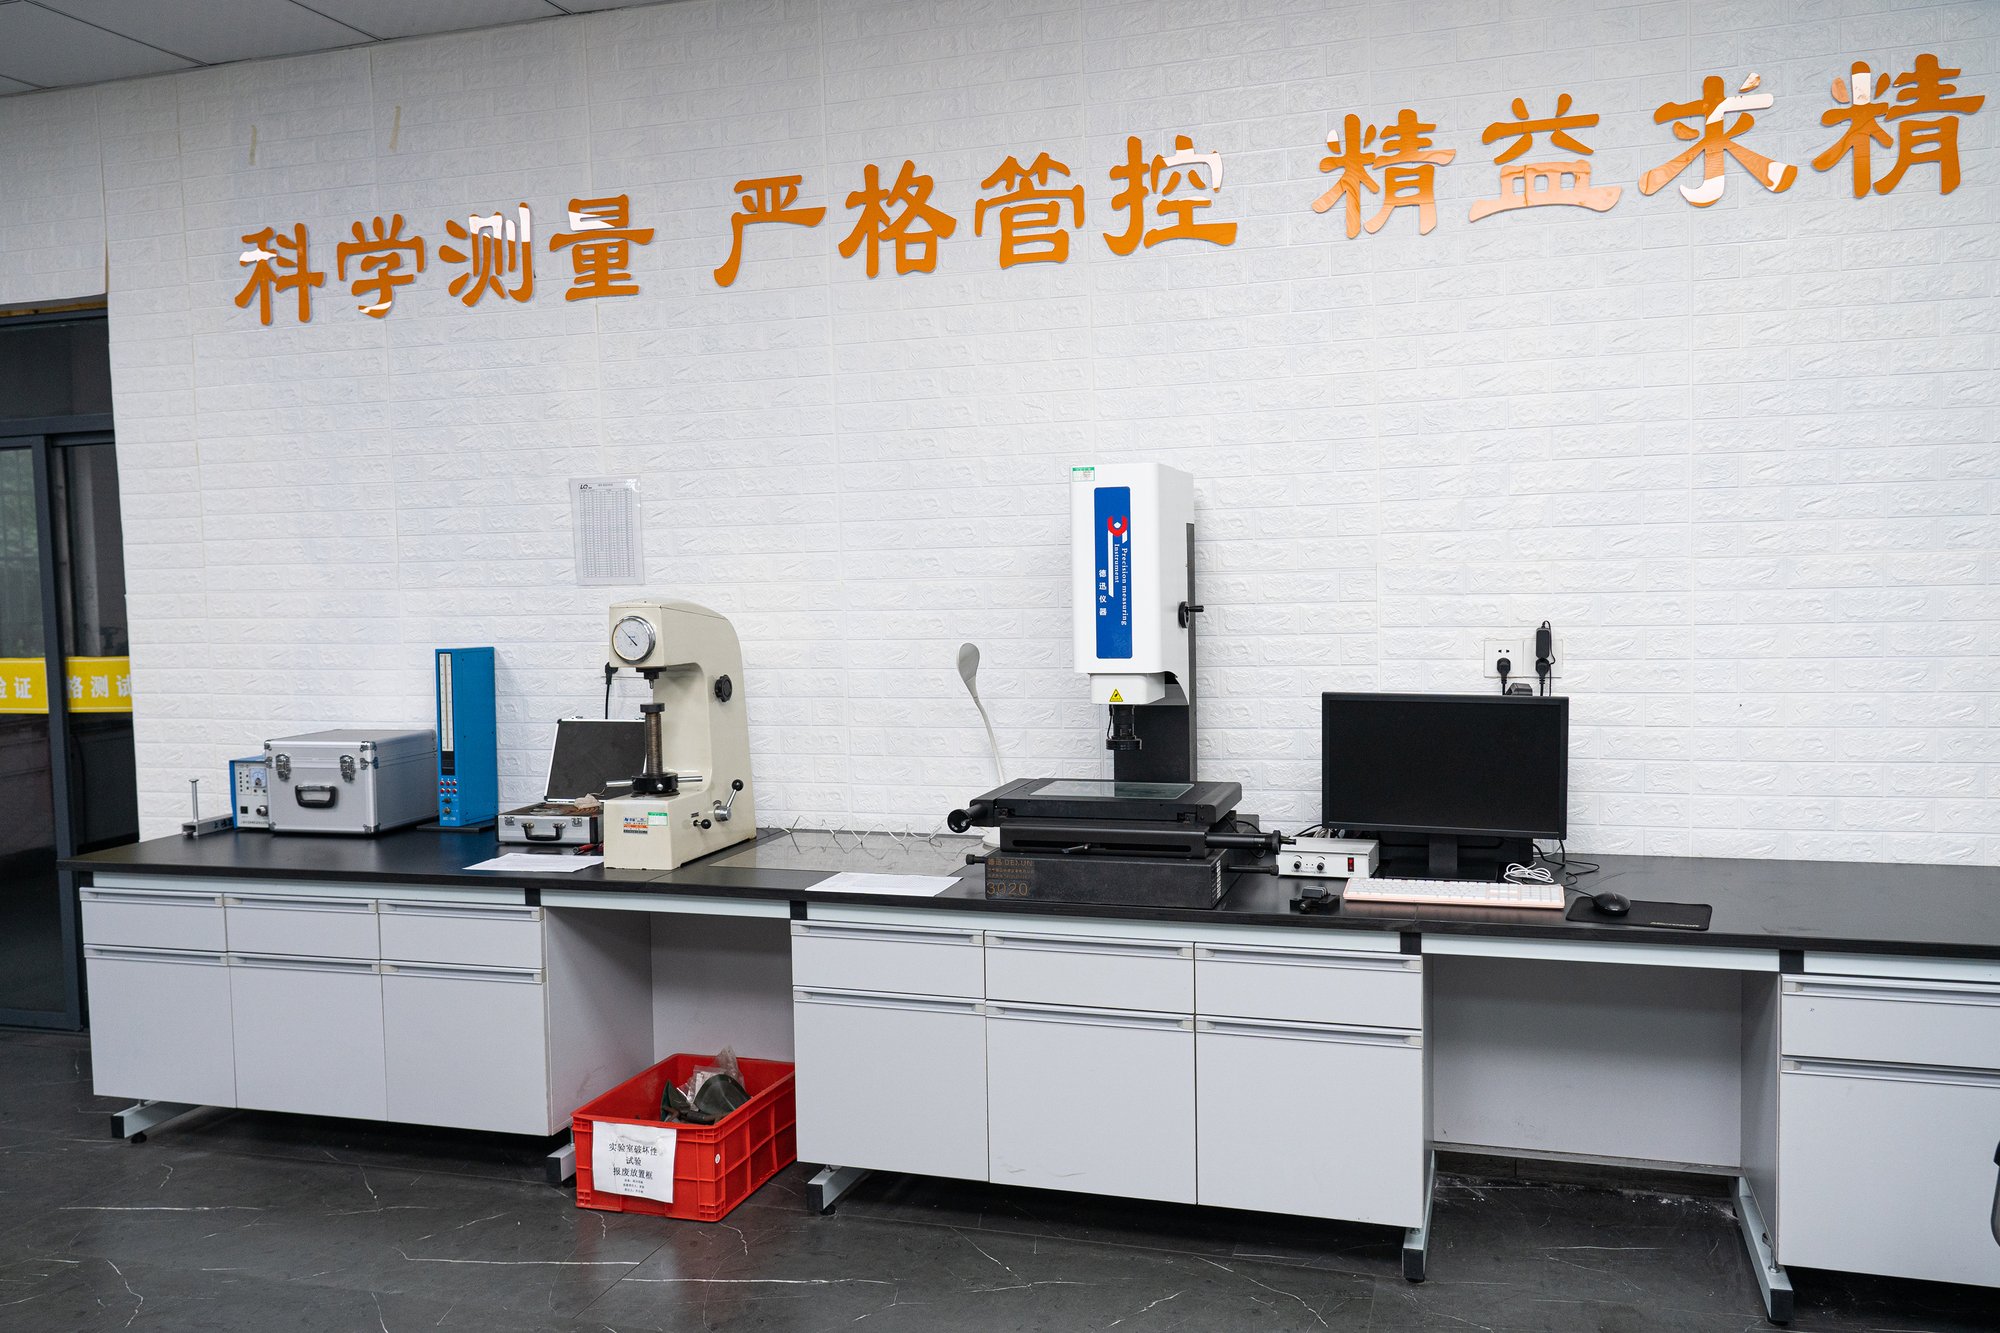
Every shipped lot carries a 3.1 inspection certificate with hardness, coating thickness and thread gauge results. Salt spray and proof load data are attached where the specification calls for them.
| Test | Standard | Our spec |
|---|---|---|
| Fatigue | Servo-hydraulic | 3 M / 6 M cycles · QA1 |
| Salt spray | ISO 9227 | Up to 1,000 h |
| Tensile / proof load | ISO 898-1 | Per property class |
| Hardness | ISO 6508 | Recorded per batch |
| Hydrogen embrittlement | Baked after plating | Per coating route |
| Thread gauge | ISO 1502 | 6g go / no-go |
FAQ
Drawings, minimums, certificates, coating choices. If something is missing, ask directly — engineering answers in English, German or Chinese.
Send the drawing and we will tell you honestly whether our tooling covers it.
Ask engineeringYes. Custom non-standard components are the core of the business — send a drawing or a sample and first articles follow in 10–15 days, with flexible MOQ.
M5 to M90, lengths from 20 mm to 3,000 mm. The largest part produced to date is an M125 × 3,000 mm T-bolt in class 8.8, 42CrMoA, weighing 296 kg.
Classes 4.6, 4.8, 5.6, 6.8, 8.8, 10.9 and 12.9 in carbon and alloy steel (42CrMoA and similar); stainless A2-50 / A4-50 / A2-70 / A4-80. Non-standard material on request.
Fatigue life is validated on production bolts on servo-hydraulic equipment — 3 million cycles for standard programmes, 6 million cycles at QA1 grade for safety-critical joints.
Heavy-duty systems are selected by corrosivity category C1–CX: hot-dip galvanising, zinc flake or DAC-type coatings, salt-spray tested up to 1,000 h to ISO 9227.
RFQ
PDF, STEP or a photo of the old part with a caliper reading — all fine. We come back with DFM comments, price breaks and a delivery date.